Parts Failing Cleanliness Inspection? A Step-by-Step Troubleshooting Guide
Introduction
The parts look clean. They passed the wash cycle, the rinse, and the dryer. Then the laboratory report comes back: particulate contamination above the limit, residual oil above specification, or a water-spot failure on the membrane. A whole lot is quarantined, a customer notification may be required, and suddenly the cleaning process that “looked fine” is the center of a quality crisis. Cleanliness failures are particularly frustrating because the cause is rarely obvious—visible cleanliness tells you almost nothing about whether a part meets a defined particle or residue standard. The most reliable way to solve them is to stop guessing and work through the cleaning system systematically. This guide gives you a structured troubleshooting approach, built around the four forces that govern every ultrasonic cleaning machine, that will lead you to the root cause of repeated inspection failures.
Start with the Failure Itself
1 Classify the Failure Before Troubleshooting
Not every cleanliness failure has the same cause, so the first step is to define exactly what the inspection found:
- •Particulate failure: too many particles, or particles too large, on the extraction membrane
- •Residual oil or grease failure: gravimetric or fluorescence testing showing organic residue
- •Fiber contamination: cloth or paper fibers present
- •Inorganic residue: salts, detergent film, or water spots
- •Location-specific failure: contamination concentrated in a specific hole or gallery
- •Intermittent failure: some batches pass and others fail without an obvious pattern
Pull the actual membrane or test data rather than relying on a verbal “it failed.” The size distribution of particles, the nature of the residue, and where contamination concentrates are diagnostic clues that point directly toward the cause.
2 Confirm the Standard and the Method
Before changing anything, verify the requirement itself. Confirm the applicable cleanliness specification (such as an OEM drawing callout referencing VDA 19 / ISO 16232), the extraction method, the analysis method, and the inspection frequency. Then confirm the extraction was performed correctly: extraction fluid volume, flushing pressure, membrane handling, and blank tests all affect results. A surprising number of “cleaning failures” are actually extraction or laboratory errors. Run a blank extraction and verify equipment calibration before you touch the washer.
The Four Forces of Cleaning: Your Troubleshooting Framework
Every cleaning result is the product of four interacting variables: mechanical energy, temperature, chemical action, and time. Cleaning engineers call this the cleaning foundation.
Force 1: Mechanical Energy
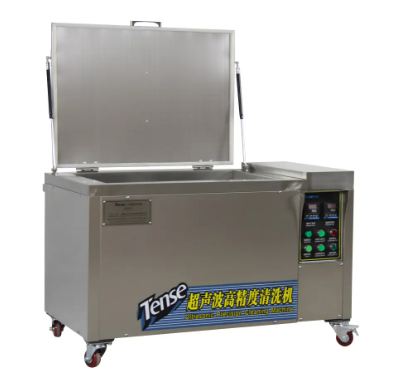
Ultrasonic cleaner TS series
Short Description:
Check:
- Are the ultrasonics actually working? Generators or transducers can fail partially. A foil test verifies energy distribution.
- Is the frequency right for the soil? 28 kHz for heavy carbon; higher frequencies for delicate parts.
- Is the power density adequate? Overloaded tanks dilute energy.
- Is the bath degassed? Fresh solution must be degassed to cavitate properly.
- Is the load blocking the energy? Avoid acoustic shadows from nested parts.
- Can solution reach internal features? Blind holes need correct orientation.
Force 2: Temperature
Heat softens grease and improves cavitation efficiency—up to a limit.
Check:
- Bath temperature: Usually 50–70°C. Verify with a thermometer.
- Rinse water: Cold rinse can re-solidify grease.
- Overheating: Above 75°C, cavitation may become less energetic.
- Pre-heat cycle: Ensure cycle starts only after reaching temperature.
Force 3: Chemical Action
The detergent breaks the bond between soil and metal. Wrong or exhausted chemistry is a common failure.
Check:
- Detergent type: Match chemistry to soil (oil, carbon, rust).
- Concentration: Verify with refractometer or titration.
- Bath exhaustion: Detergents deplete over time even if they look clean.
- pH level: Ensure it’s appropriate for the specific metal.
Force 4: Time
Cleaning requires sufficient contact time, often squeezed to hit production targets.
Check:
- Cycle length: Is it enough for the worst-case part?
- Consistency: Has the cycle been informally shortened?
- Rinse/Drain time: Adequate time to flush detergent and drain cavities.
The Fifth Element: Rinse and Dry Failures
Rinse Problems
- Dirty water redeposits oil/particles.
- Single-stage rinsing leaves residue in blind holes.
- Hard tap water leaves mineral salts (water spots).
- Stagnant tanks don’t carry contamination away.
Drying Problems
- Slow drying causes flash rust.
- Trapped water concentrates contaminants.
- Dirty air or lint cloths add new fibers.
- Bare hand handling transfers skin oils.
The Systematic Troubleshooting Sequence
- Preserve the data: Lot records and failed membranes.
- Verify the inspection: Run blanks and confirm methods.
- Interview the operator: Identify what changed in the batch.
- Check mechanical energy: Run foil tests and check orientation.
- Check temperature: Measure actual wash/rinse temps.
- Check chemistry: Test concentration, pH, and oil load.
- Check timing: Confirm durations against standards.
- Check rinse and dry: Water quality and handling.
- Change one variable at a time: Re-run controlled tests.
- Document: Update process control plans.
When Equipment Is the Root Cause
Repeated failures despite correct parameters usually indicate that the machine itself is no longer capable. Watch for degraded transducers, missing filtration, or lack of oil removal systems.
A capable industrial ultrasonic cleaner should provide uniform cavitation, heated stages, and multi-stage rinsing. Tense’s combined lifting systems built from TS-UD modules (140–2,300 liters) integrate these features for high-volume repeatability.
Conclusion
A cleanliness inspection failure is diagnostic information. Every failure reduces to one of a small number of causes. Meeting a documented cleanliness standard is a process-engineering discipline. Confirm the result consistently, and cleanliness changes from a crisis into a routine confirmation. For help, contact Tense for trials and technical support.
FAQ
Q: My parts look clean but fail particle inspection. Why?
A: Visible cleanliness tells you little about microscopic particles. Particle failures usually mean the process is not penetrating fully, the bath is saturated, or the rinse is redepositing contamination.
Q: What does VDA 19 / ISO 16232 actually require?
A: These standards define how to extract residual contamination, capture it on a filter membrane, and analyze particles by size and mass.
Q: Should we extend cycle time if parts are failing?
A: Only if inadequate time is the proven cause. It cannot compensate for failed heaters, depleted detergent, or weak transducers.
Q: How often should we change the wash bath to pass inspection consistently?
A: Tie changes to throughput and oil load rather than a fixed schedule. Monitor concentration and oil content to define measurable change criteria.